China Full Automatic Invisible Zipper Production Line
Product Overview
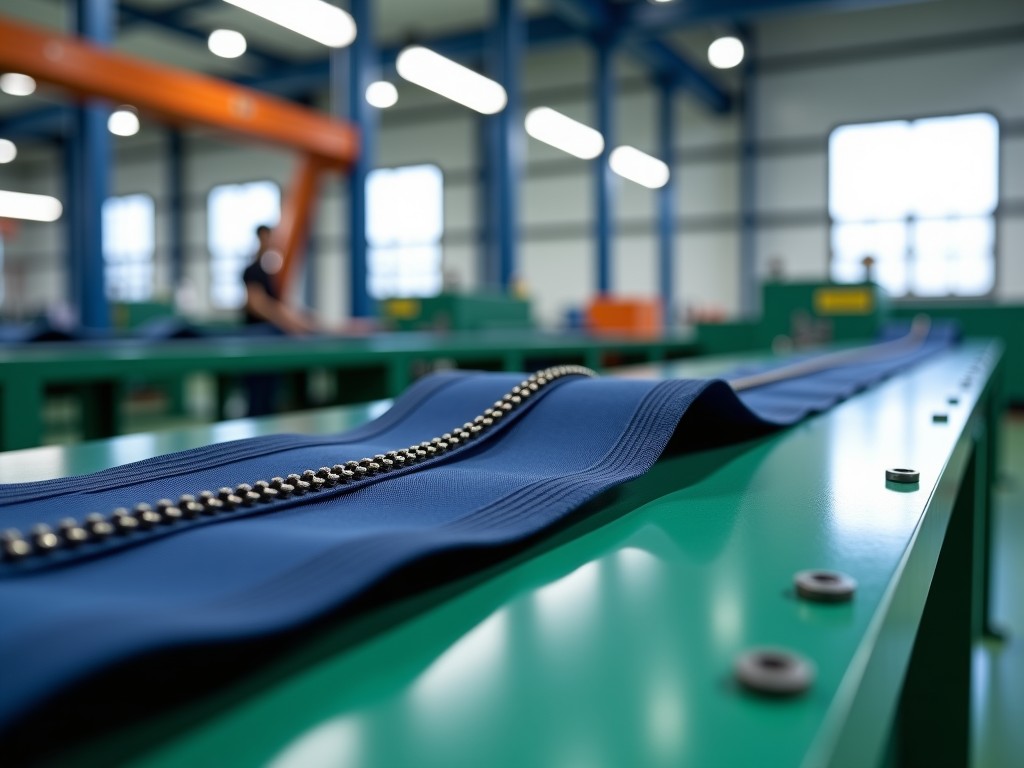
The production line integrates automated feeding of zipper tape, precise needle‑bar sewing, and inline cutting to create continuous invisible zipper strands without visible stitching on the outer surface.
Invisible zippers are formed by sewing the tape and teeth together on the inner side of the fabric, preserving a clean exterior appearance; the line maintains tape tension within ±0.2 N to prevent puckering during high‑speed operation.
Technical Specifications
Typical values are shown below; actual parameters can be adjusted according to project requirements.
| Parameter | Value | Unit |
|---|---|---|
| Maximum production speed | 180 | zipper/min |
| Zipper width range | 3–10 | mm |
| Tape feed tension control | ±0.2 | N |
| Installed power | 4.5 | kW |
| Overall dimensions (L×W×H) | 4.2×1.1×1.8 | m |
| Machine weight | 2100 | kg |
Key Features
The line incorporates engineering solutions that directly address common production challenges in invisible zipper manufacturing.
- Servo‑driven needle bar provides stitch placement accuracy within ±0.05 mm.
- Vision‑guided tape alignment system corrects lateral deviation in real time, reducing waste.
- Modular conveyor sections allow quick changeover between different zipper widths in under 5 minutes.
- Low‑tension feed rollers maintain tape stress below 0.3 N, preventing deformation.
- Integrated ultrasonic cutter delivers clean edges without burrs, eliminating secondary trimming.
- Energy‑recovery braking system recaptures up to 15 % of kinetic energy during deceleration.
Applications
In garment manufacturing, invisible zippers are essential for formal wear, dresses, and tailored outerwear where a concealed closure preserves the garment’s line.
The same technology serves luggage and sportswear producers who require durable, low‑profile closures that withstand repeated flexing without visible stitching on the exterior surface.
Quality Control
An inline vision station inspects each zipper for tooth alignment, tape twist, and stitch uniformity at the line speed, flagging any deviation beyond set tolerances.
Detected defects trigger a pneumatic reject gate that removes the faulty segment, while statistical process control logs feed data to the factory MES for trend analysis.
Customization Options
The base configuration can be expanded with optional modules to match specific product mixes or factory layouts.
- Laser cutting unit for precise length trimming of finished zipper chains.
- Ultrasonic welding station for attaching reinforced tape ends without stitching.
- Alternative feed systems for handling coated or waterproof tapes.
- Integration kit for connecting the line to existing ERP/MES platforms via Ethernet/IP.
Frequently Asked Questions
Can the production line be adjusted for different zipper tape materials?
Yes, feed rollers and tension settings are configurable for polyester, nylon, or coated tapes; material changeover typically requires <30 minutes.
What information is needed to prepare a quotation?
Required details include target zipper width, desired output speed, tape type, and any optional modules such as laser cutting or welding.
How is quality inspection performed during operation?
A high‑speed camera system inspects each zipper for tooth alignment, tape twist, and stitch consistency; results are logged and used to trigger automatic reject if limits are exceeded.
Contact Us
For technical details, pricing, or to arrange a factory visit, please reach out to our sales team.
Request a quote