Factory Direct Metal Zipper Turnkey Production Line
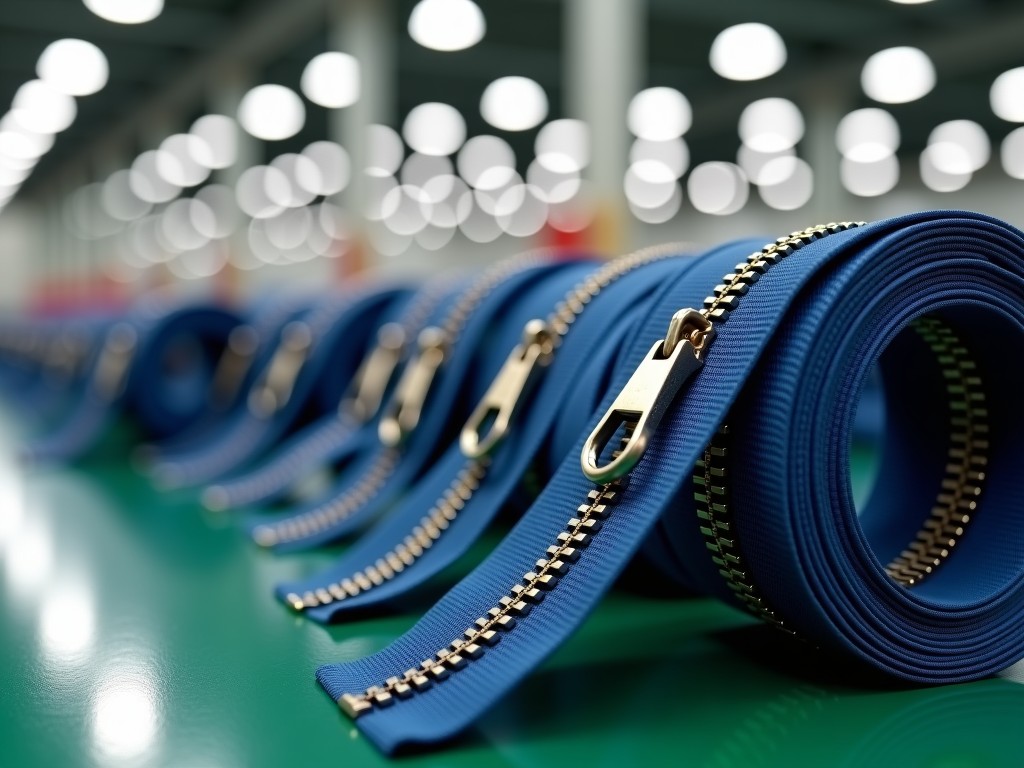
This turnkey line integrates coil feeding, precise roll forming, zipper teeth formation, slider insertion, and final winding into a single continuous process that outputs finished metal zippers ready for downstream sewing or molding operations.
System Overview
The line consists of five primary stations: uncoiling, forming, teeth insertion, slider assembly, and winding. Each station is linked by servo‑driven conveyors that maintain constant pitch and allow independent speed tuning for product changeover.
- Uncoiling Station: Motor‑driven pay‑off with dancer arm maintains tension within ±2 N.
- Forming Station: Four‑roll set shapes the metal strip into the zipper base profile with thickness tolerance ±0.02 mm.
- Teeth Insertion Station: High‑speed rotary dies form interlocking teeth at a rate up to 120 strokes/min.
- Slider Assembly Station: Precision pick‑and‑place units insert sliders with positional accuracy ±0.1 mm.
- Winding Station: Controlled take‑up spools wind finished zippers at constant tension to prevent deformation.
Technical Specifications
| Parameter | Typical Value | Customizable Range |
|---|---|---|
| Line Speed | 30‑45 m/min | 20‑60 m/min (drive adjustment) |
| Zipper Width | 5 mm (standard) | 3‑12 mm (tooth pitch adjustable) |
| Material Thickness | 0.12‑0.25 mm (steel or brass) | 0.08‑0.30 mm (depending on alloy) |
| Power Consumption | ≈12 kW (average) | 9‑15 kW (based on speed and material) |
| Footprint (L×W×H) | 6.2 m × 1.8 m × 2.2 m | Modular extensions available |
Key Modules and Functions
- Uncoiling Station: Motor‑driven pay‑off with dancer arm maintains tension within ±2 N.
- Forming Station: Four‑roll set shapes the metal strip into the zipper base profile with thickness tolerance ±0.02 mm.
- Teeth Insertion Station: High‑speed rotary dies form interlocking teeth at a rate up to 120 strokes/min.
- Slider Assembly Station: Precision pick‑and‑place units insert sliders with positional accuracy ±0.1 mm.
- Winding Station: Controlled take‑up spools wind finished zippers at constant tension to prevent deformation.
Customization Options
- Zipper width: 3 mm to 12 mm (tooth pitch adjustable)
- Tooth profile: Y‑type, coil‑type, invisible, or custom geometry via interchangeable rollers
- Material: carbon steel, stainless steel, brass, zinc‑alloy; thickness 0.08‑0.30 mm
- Slider type: automatic lock, semi‑automatic, non‑lock; size range 3‑8 mm
- Line layout: straight, L‑shaped, or Z‑shaped to fit facility constraints
- Additional modules: pre‑coating, post‑plating, or inline inspection stations
Quality Control Philosophy
Inline laser gauges monitor tooth height and width every 0.5 m, feeding data to a PLC that rejects out‑of‑spec segments automatically. A vision system checks slider orientation and presence with 99.9 % detection rate. Periodic tensile tests on random samples verify that finished zippers exceed 150 N pull‑strength, meeting EN 13356 and ISO 9001‑2015 requirements.
Applications
Metal zippers produced on this line meet the tensile strength requirements (>150 N) for heavy‑duty workwear, automotive interior trim, outdoor gear, and military equipment. The ability to run brass or stainless‑steel strips enables corrosion‑resistant fasteners for marine and industrial environments, while the tight thickness tolerance ensures consistent sewing machine feed and low needle wear.
Frequently Asked Questions
Q: Can the line be configured for different tooth profiles?
A: Yes, the forming rollers are interchangeable; common profiles include Y‑type, coil‑type, and invisible, with custom geometries available upon request.
Q: What information is required before quotation?
A: Desired zipper width, material type and thickness, tooth profile, slider type, target line speed, and any additional modules such as coating or inspection.
Q: How is quality inspected during production?
A: Inline laser gauges monitor tooth dimensions, a vision system verifies slider placement, and a reject mechanism removes non‑conforming sections without stopping the line.
Q: What packaging methods are available for the finished zippers?
A: Standard options include spool winding, flat‑pack in cartons, or custom reels; all packaging includes anti‑static lining and humidity‑controlled barriers as needed.
Q: What is the typical production lead time?
A: For a standard configuration, lead time is 8‑10 weeks after receipt of purchase order and detailed specifications; custom modules may extend this period.