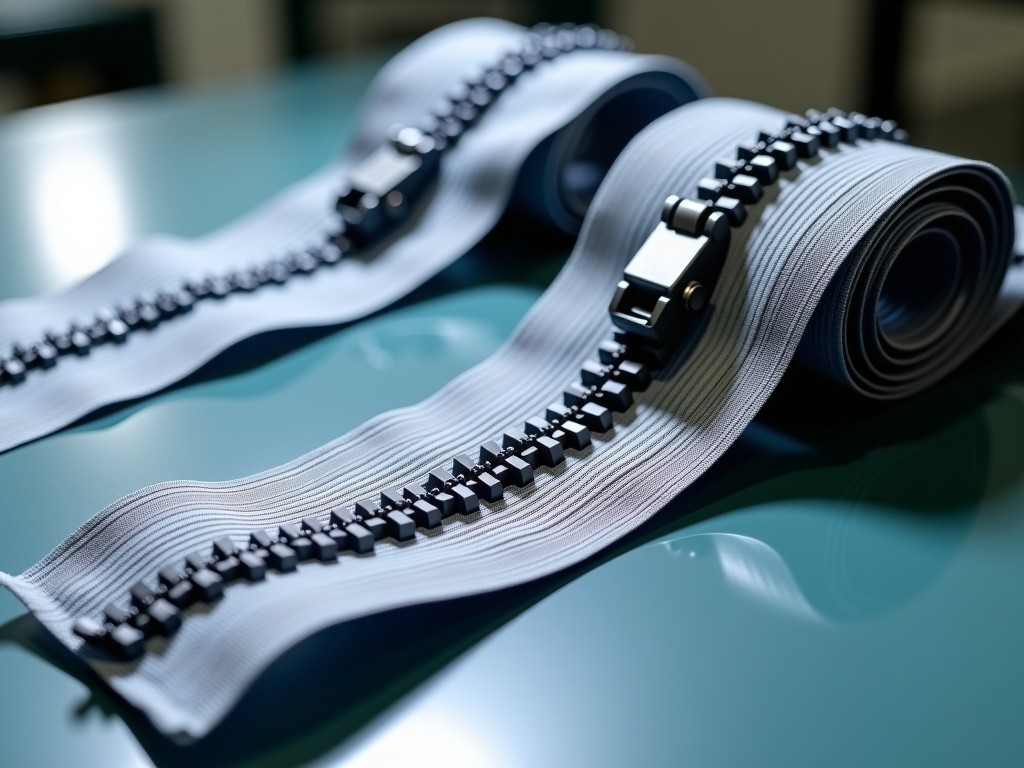
Bulk Nylon Zipper Production Line Manufacturer
A bulk nylon zipper production line integrates material feeding, heating, molding, cooling, cutting, and winding subsystems to produce continuous lengths of nylon zipper tape and teeth at high throughput. The line is engineered for consistent dimensional control across wide widths and varying coil geometries, enabling manufacturers to meet large‑volume orders with minimal changeover time.
Core Technical Specifications
| Parameter | Typical Value | Unit | Notes |
|---|---|---|---|
| Line speed | Up to 120 | m/min | Adjustable via servo drive |
| Number of molding heads | 4–8 | pcs | Configurable per product width |
| Zipper tape width range | 3–25 | mm | Custom dies available |
| Installed power | 180–250 | kW | Dependent on head count |
| Control system | PLC + HMI | – | Recipe management included |
Main Process Stages
- Nylon granulate is dried and fed to a single‑screw extruder for melt homogenization.
- The melt is split and directed to molding heads where zipper teeth are formed under controlled pressure and temperature.
- Simultaneously, tape is extruded, cooled, and pulled to synchronize with tooth formation.
- Teeth and tape are joined in a continuous bonding zone, then cooled to set dimensions.
- The finished zipper tape is cut to length, wound onto spools, and subjected to inline inspection.
Mechanical and Electrical Characteristics
| Characteristic | Value | Unit |
|---|---|---|
| Extruder screw diameter | 90 | mm |
| Molding cavity pressure | 150–200 | bar |
| Drive motor type | Servo, 7.5 kW per head | – |
| Power supply | 380 V, 3‑phase, 50 Hz | – |
Applications in Textile Manufacturing
The line serves manufacturers that require long continuous lengths of nylon zipper for garments, luggage, and industrial fabrics. By producing zipper tape and teeth in a single integrated process, it eliminates the need for separate tape extrusion and tooth molding lines, reducing handling steps and minimizing length‑related tolerances that can cause misalignment during garment assembly.
Customization Options
- Number of molding heads adjustable from 2 to 12 to match width and output requirements.
- Die sets available for coil, molded, or invisible zipper profiles.
- Optional inline lubrication or coating stations for enhanced tape smoothness.
- Choice of control architectures: basic PLC or advanced SCADA with remote monitoring.
- Variable take‑up spool sizes ranging from 200 m to 2000 m capacity.
Quality Assurance and Testing
Inline monitoring includes laser diameter measurement of tape thickness (±0.02 mm), tooth pitch verification (±0.05 mm), and tensile strength testing of finished zipper (≥30 N/mm). Periodic off‑line sampling is conducted for zipper pull strength and colorfastness to ensure compliance with OEM specifications. All data are logged and traceable to production batch for audit purposes.
Frequently Asked Questions
Yes, the extruder screw temperature profile and molding heating zones can be re‑configured for polyester, polypropylene, or blends, subject to material supplier validation.
Desired tape width, zipper type, target line speed, required power supply details, and any special features such as coating or inline inspection.
Laser gauges monitor tape dimensions in real time, while load cells measure tensile strength on cut samples; alarms trigger if values exceed preset tolerances.
Lead times range from 14 to 20 weeks depending on the degree of customization and component availability.
Contact for Technical Inquiry
For detailed technical data, layout drawings, or to discuss specific project requirements, please send an inquiry using the link below.
Send technical inquiry