Wholesale Waterproof Plastic Zipper Machine
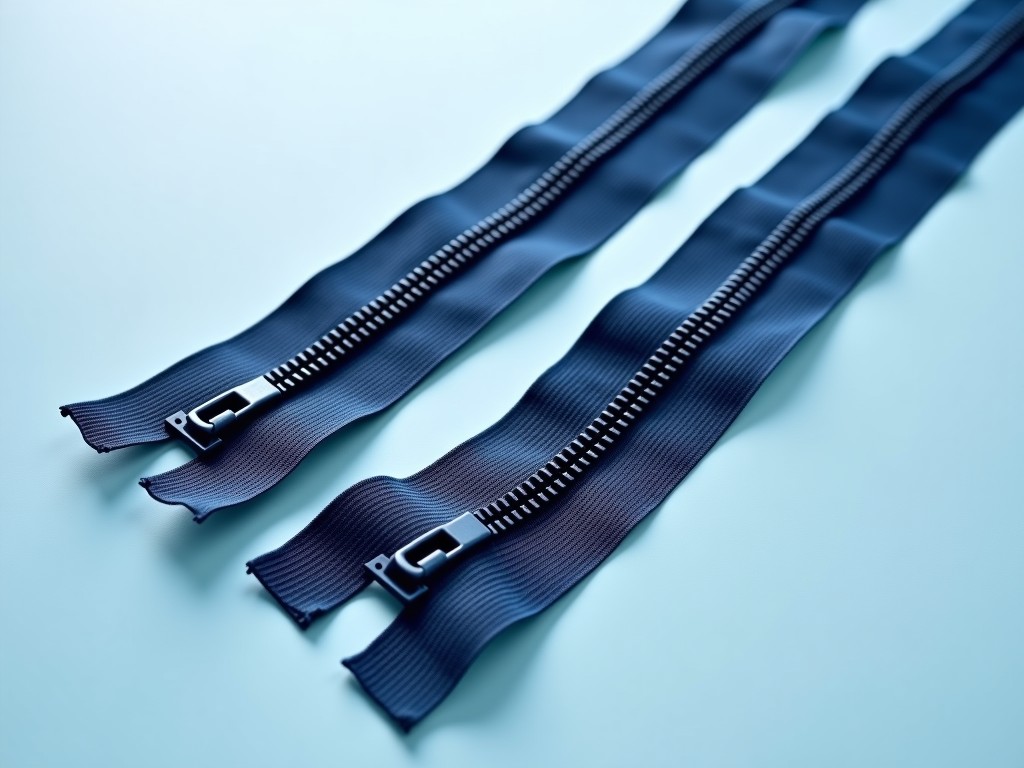
This equipment produces continuous lengths of PVC‑coated polyester zipper tape that maintains a watertight seal under pressure. The machine integrates extrusion, coating, and zipper formation in a single line, allowing manufacturers to supply sealed closures for outdoor gear, marine equipment, and protective apparel.
Machine Overview
Three synchronized modules form the core: a twin‑screw extruder that melts and homogenizes the PVC compound, a flat‑die coating head that applies a uniform 0.18 mm thick layer onto a polyester base fabric, and a rotary zipper molding station that interlocks the tape into a continuous chain with a pitch of 5 mm. All modules share a common drive shaft rated for 150 kW torque, enabling stable operation at speeds up to 30 m/min.
Key Technical Specifications
| Parameter | Typical Value | Adjustable Range |
|---|---|---|
| Extruder screw diameter | 45 mm | 40–50 mm |
| Coating thickness | 0.18 mm | 0.12–0.25 mm |
| Zipper pitch | 5 mm | 4–6 mm |
| Maximum line speed | 30 m/min | 20–40 m/min |
| Installed power | 150 kW | 120–180 kW |
Operating Principles
Polymer pellets are fed into the extruder where shear heating raises the melt temperature to 180 °C. The melt pressure, monitored by a transducer, is maintained between 8 and 12 bar to ensure consistent output. The coated fabric exits the die at a temperature of 140 °C, allowing rapid cooling on a chilled roller set to 25 °C, which solidifies the PVC layer without inducing residual stress.
The rotary molding station uses a set of interlocking pins shaped to the zipper profile. As the tape passes, the pins engage and disengage at a frequency synchronized to the line speed, forming the teeth and pockets. A pneumatic tensioner keeps the tape under 0.5 N of lateral force to prevent misalignment during molding.
Materials and Construction
The base fabric is a 150 denier polyester filament yarn with a tensile strength of 55 MPa and an elongation at break of 22 %. The PVC compound incorporates 12 % phthalate‑free plasticizer, 5 % UV stabilizer, and 2 % anti‑microbial additive, providing a Shore A hardness of 85 and a water‑absorption rate below 0.2 % after 24 h immersion.
Machine frames are constructed from S355 steel with a powder‑coated finish rated for 500 h salt‑spray resistance. All moving shafts are supported by double‑row tapered roller bearings with a dynamic load rating of 32 kN, ensuring a mean time between failures (MTBF) exceeding 4,000 h under continuous operation.
Applications in Industrial Sealing
Waterproof zippers produced on this line are used where a flexible barrier must resist hydrostatic pressure. In marine dry‑suits, the zipper maintains seal integrity at depths up to 30 m, corresponding to a pressure differential of 0.3 MPa. In outdoor backpacks, the same zipper resists rain ingress equivalent to a 100 mm/hour rainfall rate for 8 h without leakage.
Additional sectors include medical protective covers, where the zipper must withstand sterilization cycles at 121 °C, and automotive under‑body shields, where resistance to oil and diesel fuels is required. The PVC formulation’s swelling ratio in diesel is less than 3 % after 48 h exposure, meeting typical OEM specifications.
Customization Options
- Adjustable die width for tape widths from 20 mm to 80 mm.
- Optional hot‑air pre‑heater to raise fabric temperature to 160 °C for improved adhesion.
- Alternative zipper profiles: coil, molded tooth, or invisible.
- Integration of a laser‑etched logo station operating at 10 W pulse frequency.
- Custom control PLC programming for recipe storage of up to 50 parameter sets.
Quality Control and Testing
Each production lot undergoes inline width measurement using laser triangulation with an accuracy of ±0.02 mm. Zipper tensile strength is sampled every 30 m using a constant‑rate‑of‑extension tester; the specification requires a minimum of 25 N per 10 mm width. Water ingress is verified by a static pressure test at 0.5 bar for 5 min, with no detectable leakage using a dye‑penetration method.
Final inspection includes visual inspection under 500 lux illumination for defects such as fish‑eyes, bubbles, or mis‑aligned teeth, limited to a maximum of 2 defects per 100 m. All test data are logged to the Manufacturing Execution System (MES) and made available to customers upon request.
Frequently Asked Questions
Can the machine be configured for different zipper pitches?
Yes, the rotary molding station is interchangeable; pitches from 4 mm to 8 mm are available by changing the pin set and adjusting the drive ratio.
What information is required before a quotation?
Needed details include desired tape width, coating thickness, zipper profile, line speed, and any special additives (e.g., fire‑retardant, anti‑static). Providing a sample of the base fabric helps us validate adhesion parameters.
Which materials are available for the base fabric?
Standard offerings are polyester filament, nylon 6,6, and aramid blends. Custom fabrics such as UHMWPE‑coated polyester can be accommodated upon request.
How is quality inspected?
Inline laser width monitoring, periodic tensile testing, and static pressure water‑ ingress checks are performed. Final visual inspection follows ISO 9001‑based AQL limits.
What packaging methods are available?
Finished zipper tape is wound onto corrugated cores with inner diameter 76 mm, wrapped in polyethylene shrink film, and placed in palletized cartons. Custom labeling and barcoding can be added.
How are export shipments protected?
Pallets are strapped with polyester bands, corner protectors are applied, and the entire load is covered with a waterproof tarp. Containerized shipments include desiccant packs to maintain relative humidity below 50 %.
What is the typical production lead time?
Lead time ranges from 4 to 6 weeks after receipt of the technical data sheet and deposit, depending on the degree of customization.
How are samples arranged?
Sample lengths of 5 m are produced under the customer’s specified parameters and shipped via express courier with tracking. Sample preparation typically takes 3 business days.